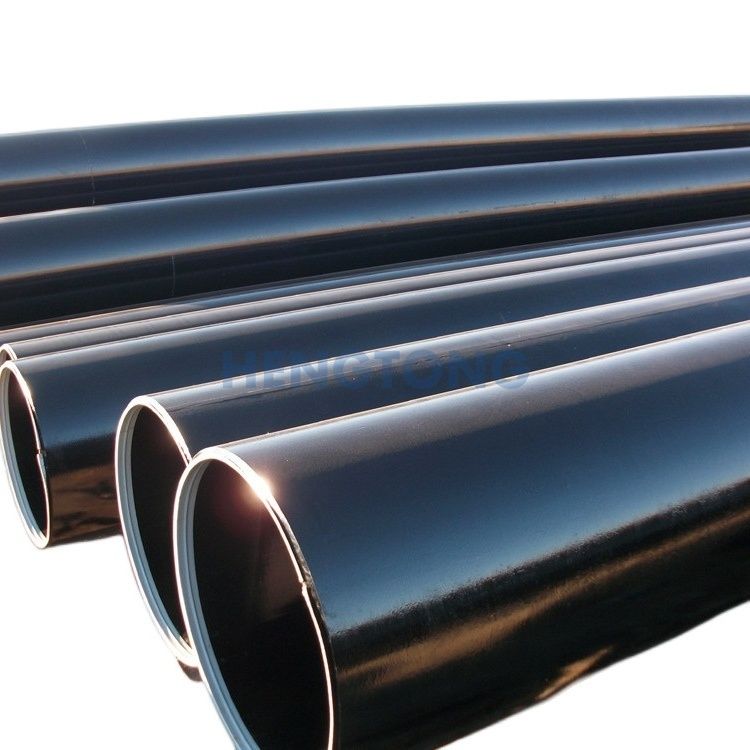
ASTM A691 2 1/4CR CL42 Alloy Steel EFW Pipe
ASTM A691 2-1/4 铬 CL42 级电熔焊合金钢管
Steel Pipes / Longitudinal Submerged Arc Welded Steel Pipe
ASTM A691 2 1/4CR CL42 Alloy Steel EFW Pipe
ASTM A691 2-1/4 铬 CL42 级电熔焊合金钢管
Need a quotation or catalog for this product? Send an inquiry — we will reply as soon as possible.
Get a Quote →Product Description
ASTM A691 2 1/4CR CL42 Alloy Steel EFW Pipe
1. Concise Copyable Version
Our ASTM A691 2 1/4CR CL42 electric fusion welded alloy steel pipes are manufactured from 2.25Cr-1Mo heat-resistant alloy, matching A335 P22 material grade for high-temperature & high-pressure working conditions. Strict chemical composition and mechanical property limits are implemented to guarantee high-temperature creep resistance and oxidation stability. Full normalized + tempered heat treatment and 100% non-destructive weld inspection are mandatory during production, complying with ASME testing codes. Suitable for long-term service at 450–600°C, widely adopted in thermal power steam pipelines, petrochemical hydrogenation facilities and nuclear auxiliary piping. We provide complete heat treatment documents and third-party inspection certificates, with customizable diameter, wall thickness and anti-corrosion coating schemes. Standard operating temperature cap is 540°C; standardized on-site welding and periodic thickness inspection are required for long-term safe operation.
2. Detailed Copyable Version
ASTM A691 2 1/4CR CL42 High Temp High Pressure EFW Alloy Pipe
ASTM A691 covers fusion welded steel tubes dedicated to extreme high-temperature and high-pressure industrial piping systems, including carbon steel and chrome-moly alloy variants. Our 2 1/4CR CL42 grade pipe adopts premium 2¼Cr-1Mo alloy base metal, chemically equivalent to A335 P22, engineered to sustain continuous service under harsh thermal environments up to 600°C.
Strict Raw Material Chemical & Mechanical Standards
- Chemical Composition Control
- Chromium: 2.00%–2.50%, Molybdenum: 0.90%–1.10%
- Carbon ≤0.15%, Sulfur & Phosphorus each capped at 0.025% to reduce brittleness and improve weldability
- Mechanical Performance Benchmarks
- Minimum yield strength: 310MPa (45ksi), minimum tensile strength: 585MPa (85ksi)
- Elongation ≥20%, maximum hardness restricted to 250HBW
- Room-temperature Charpy V-notch impact energy ≥54J; certified 540°C high-temperature tensile performance to validate high-temperature structural stability
Standardized Manufacturing & Post-Weld Processing
All pipes are produced via electric fusion welding (EFW) followed by full-cycle heat treatment:
- Normalization heating at 900–1000°C to homogenize internal metal grain structure
- Primary tempering at 680–760°C to relieve forming stress
- Extra post-weld heat treatment (PWHT) at 700–760°C applied to all welded joints Every weld joint undergoes full-coverage radiographic (RT) or ultrasonic (UT) non-destructive testing in line with ASME inspection specifications to eliminate internal welding flaws. Dimensional tolerance rules: outer diameter deviation ±0.5%, wall thickness tolerance +19% / -8%.
Core Application Fields
This chrome-moly alloy pipe is the preferred material for equipment operating under 450°C to 600°C thermal loads:
- Thermal power plants: high-pressure superheated steam trunk pipelines
- Petrochemical refineries: hydrogenation reactor circulation piping
- Nuclear power auxiliary circulation pipelines Its outstanding anti-creep and high-temperature oxidation resistance avoids structural deformation under long-term high-temperature pressure load. We supply complete heat treatment records and third-party inspection reports for full material traceability.
Critical Installation & Service Guidelines
- Welding Specification Matching On-site fabrication must replicate factory welding procedures, with mandatory preheating before welding and matching alloy filler metals compatible with the 2¼Cr-1Mo substrate.
- Service Temperature Restriction The safe continuous operation ceiling stands at 540°C. Extended service above this threshold triggers molybdenum precipitation inside the alloy matrix, weakening creep resistance and shortening overall service lifespan.
- Corrosion Protection Upgrade Though the Cr-Mo alloy delivers inherent oxidation resistance, supplementary anti-corrosion lining or coating is required for ultra-corrosive working media to block intergranular corrosion.
- Regular Periodic Inspection After 3–5 years of continuous operation, wall thickness and hardness testing must be carried out to track material aging and schedule timely pipe replacement.
Price Influencing Factors
Total cost fluctuates based on raw alloy plate market prices, precision heat treatment and full NDT quality control procedures. Larger outer diameters, thicker wall schedules and longer single pipe lengths raise raw material consumption and production complexity, resulting in higher unit pricing. Custom anti-corrosion coating and third-party certification also adjust final quotation.
Rewritten SEO Hot Tags
ASTM A691 2 1/4CR CL42 alloy steel pipe, China high temperature EFW pipe manufacturer, 2.25Cr1Mo heat resistant welded tube, A335 P22 equivalent steam pipeline, petrochemical hydrogenation alloy piping, thermal power high pressure steel pipe, nuclear auxiliary chrome moly pipe, ASME standard NDT tested alloy tube, custom size high temperature resistant steel pipe, anti creep fusion welded alloy pipe